What It Is Built For vs. When to Choose Another Configuration
Target Products & Production Duty
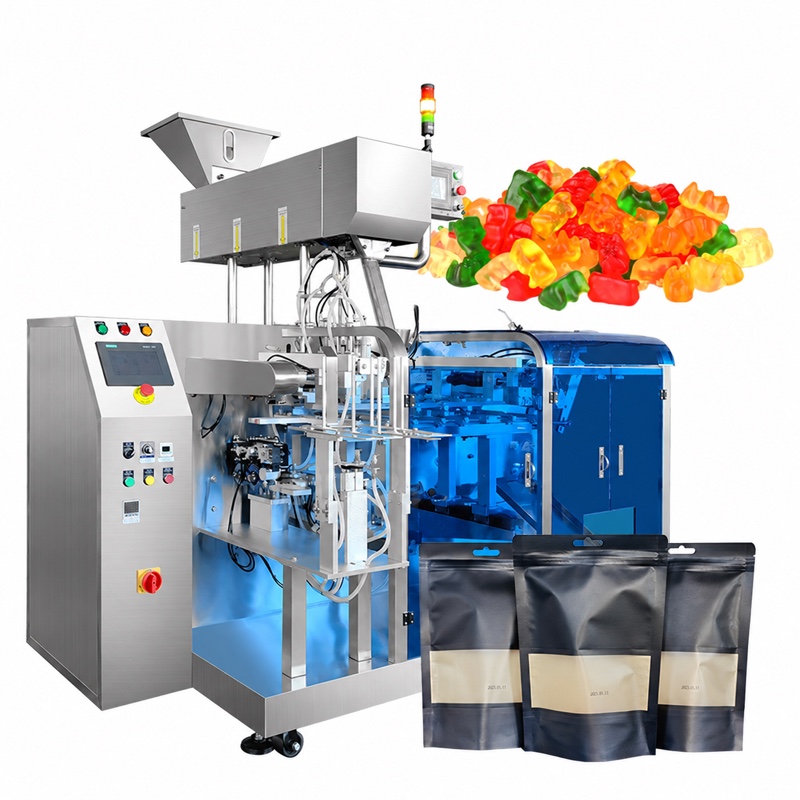
- Confectionery and functional gummy brands packing pectin/gelatin gummies, vitamin chews, and sour jellies into retail resealable stand-up zipper pouches (90–210 × 110–330 mm).
- Secondary multipack lines collating 10–40 sealed konjac sticks or mini jelly cups into family-size stand-up doypacks at 20–70 bags/min.
- Brands needing crisp shelf-standing gussets and press-to-close zippers without vertical forming-collar creases.
Better-Matched Sibling Configurations
Economical rollstock pillow or gusset bags of gummies at 30–70 bags/min without premade zipper pouches
Large Gummy Candy VFFS & Anti-Stick Weigher Line →Pre-spouted corner/top screw-cap pouches filled with liquid drinking jelly (10–15 bags/min)
LV-160 Automatic Spout Pouch Jelly Filler →Primary multi-lane stick-pack or 4-side sachet filling of liquid/hot-fill gel
Multi-Lane Konjac & Energy Gel Stick Machine →
Specification Table (Metric & Imperial)
| Parameter | Metric Specification | Imperial Equivalent | Operating Condition & Verification Note |
|---|---|---|---|
| Model | LV-210 | — | LINEVO T04 premade pouch packaging series. |
| Bag Width | 90–210 mm | 3.54–8.27 in | The forming set or change parts are made for each pack size you run. |
| Bag Length | 110–330 mm | 4.33–12.99 in | The forming set or change parts are made for each pack size you run. |
| Packing Speed | 20–70 bags/min | — | Depends on the product, fill weight, and pack size (apply 0.70–0.85 shift OEE). |
| Power & Voltage | 3.5 kW · 220V, 50/60Hz | — | Give voltage, phase, and frequency at your site; quotation states electrical configuration. |
| Machine Weight | 900 kg | 1,984 lb | Net machine weight; shipping weight and crate size are stated with the order. |
| Machine Size | 2150 × 1350 × 1300 mm | 84.6 × 53.1 × 51.2 in | Length × width × height; layout drawing in quotation shows complete floor space with weigher. |
Shift Production Reality Note: Listed cycle speeds depend on container or bag volume, target fill weight, and material flow characteristics. For multi-shift plant planning, multiply nominal run rate by a 0.70–0.85 shift OEE factor (accounting for film/label splices, hopper refills, and routine cleaning) and confirm exact speed with your samples during Foshan FAT.
What Is Included vs. What We Review With You
Core Station Scope
- Automatic premade pouch magazine retrieval, vacuum suction + zipper opening station, and heat-sealing/cooling bars
- Finished pouch discharge chute within 2150 × 1350 × 1300 mm base machine frame
Reviewed Against Your Samples & Plant
- Application, format gripper/opener tooling, and upstream multihead weigher (anti-sticking dimpled buckets for oiled/sugar-sanded gummies) or liquid filler
- Ribbon/TIJ date-coding station, no-open/no-fill sensor interlocks, and Z-bucket elevator platform
Verified Electrical, Sensing & Pneumatic BOM
PLC Motion & Sequence Controller
Main programmable logic controller coordinating multi-lane rotary piston dosing, film/cup indexing, jacket heating, and sealing interlocks.
Rotary Encoder, Control Relays & 24V Switching Power Supply
Phase-angle timing feedback, cabinet switching relays, and regulated 24V DC power supply across multi-lane stick, sachet, and cup stations.
HMI Color Touchscreen & Variable Frequency Drive (VFD)
Multi-recipe touchscreen terminal storing lane dose/temperature profiles and inverter motor speed control for main drives and conveyors.
Pneumatic Cylinders, Solenoid Valves, Vacuum Gauge & FRL Unit
Suck-back anti-drip nozzle actuators, cross-sealing cylinders, manifold valves, pouch-opening vacuum gauge, and air preparation unit.
Representative electrical, sensing, and pneumatic hardware fitted on LINEVO packaging configurations; exact part series or project-specified alternatives are itemized in your written quotation BOM.
How It Works & Mechanical Countermeasures to Common Line Failures
- 01Automatic Bag Retrieval
Vacuum suction arms pick flat premade stand-up or zipper pouches cleanly from the horizontal magazine.
- 02Top & Zipper Track Opening
Dual vacuum pads and mechanical zipper-opening jaws separate both the pouch mouth and press-to-close zipper track.
- 03Synchronized Product Fill
Gummies, jelly beans, or sealed mini jelly cups/sticks drop cleanly through a funnel that shields the zipper track from sugar dust.
- 04Heat Sealing, Cooling & Output
Heat bars fuse the top seal above the tear notch, cooling bars flatten the seam, and finished stand-up pouches discharge.
Production Floor Failure Modes & LINEVO Countermeasures
Unopened Zipper Pouches Dumping Gummies Onto the Shop Floor
Floor Risk: Static cling or stiff matte-varnish doypacks occasionally resist suction cups, causing blind fillers to dump expensive vitamin gummies onto machinery.
Mechanical Countermeasure: Dedicated mechanical zipper-opening jaws separate the zipper track positively before triggering upstream weigher discharge.
Citric Sour Sugar Sand Fouling Press-to-Close Zipper Tracks
Floor Risk: Loose sour sugar crystals lodging inside zipper grooves prevent consumers from resealing bags and contaminate top heat seals.
Mechanical Countermeasure: Diving fill funnels extend past the zipper track during gummy discharge so top seal margins stay clean.
Wrinkled Top Seams on Wide 180–210 mm Heavy Multipack Doypacks
Floor Risk: Heavy 500 g–1 kg jelly-cup multipacks sag in weak grippers, buckling the top header before heat sealing.
Mechanical Countermeasure: Rigid pouch grippers and two-stage heat + cooling bar consolidation iron flat, retail-grade header seams.
Oiled or Pectin Gummies Bridging in Upstream Scales
Floor Risk: Sticky confectionery slows net LV-210 speed well below dry mechanical capability.
Mechanical Countermeasure: LINEVO pairs LV-210 with embossed anti-sticking multihead weighers verified on your gummy samples in Foshan.
Comparing Quotations? Check These 5 Things
Multiply cycle rate (20–40 cuts/min) by lane count and a realistic 0.70–0.85 shift OEE factor accounting for hot-fill hopper replenishment, parent reel splices, and CIP sanitation.
Verify whether double-walled jacketed heating, mixing paddles, rotary-valve piston dosing, and pneumatic suck-back shut-off nozzles are sized for your gel viscosity and particulate size.
Confirm product-contact steel grade for acidic fruit gels, electrical heater load (kW, voltage/phase), and dry compressed air consumption (0.6–0.8 MPa) on the written scope sheet.
Check parent rollstock maximum width (420 / 500 / 700 / 980 mm), lane pitch, tear-notch punch geometry, and cup cavity rings against approved dieline drawings before plate engraving.
Require a filmed Foshan FAT running viscous gel or gummy samples at target fill temperature to verify zero seal-zone stringing, weight uniformity across lanes, and burst resistance.
From Sample Audit to Foshan FAT & Export Commissioning
- 01Sample Audit
Send physical containers, pouches, lids, film reels, or product specs to Foshan so engineers verify dimensions, flow behavior, and station geometry.
- 02Written Scope Freeze
Confirm exact model/lane count, included vs. project-reviewed modules, electrical/air utilities, and format parts in the technical quotation.
- 03Foshan Fabrication & Wiring
CNC machining, stainless frame assembly, PLC/HMI programming, and inline station synchronization inside LINEVO's 15,000+ m² Foshan plant.
- 04Foshan FAT Run Before Shipment
Full-speed trial on sample materials verifying registration, dosing/vacuum stability, seal integrity, and fault interlocks on video or in person.
- 05Export Crating & Commissioning
Fumigation-free export crating, English schematics, parameter backups, wear-part list, and remote video or scheduled on-site commissioning.
Frequently Asked Questions
Can the LV-210 also fill liquid drinking-jelly into premade stand-up pouches?
Yes—within the LV-210 platform family (which also includes premade juice and milk/beverage configurations), pairing piston liquid nozzles instead of a gummy weigher fills liquid stand-up pouches across 90–210 × 110–330 mm.
How fast does LV-210 run on resealable zipper gummy bags in real shifts?
Published range is 20–70 bags/min depending on pouch dimensions, zipper opening dwell, and gummy dump settle time; plan 0.70–0.85 shift OEE in our Jelly Output Calculator (/tools/jelly-line-output-calculator/).
What pouch features work on LV-210?
Stand-up bottom-gusset doypacks, flat 3-side-seal bags, press-to-close zippers, euro-slot hang holes, and tear notches within 90–210 mm width and 110–330 mm length.