What It Is Built For vs. When to Choose Another Configuration
Target Products & Production Duty
- Beverage and functional snack brands filling pre-spouted center-neck or corner-spout pouches with konjac drinking jelly, fruit puree, energy gel, or household liquids at 10–15 bags/min.
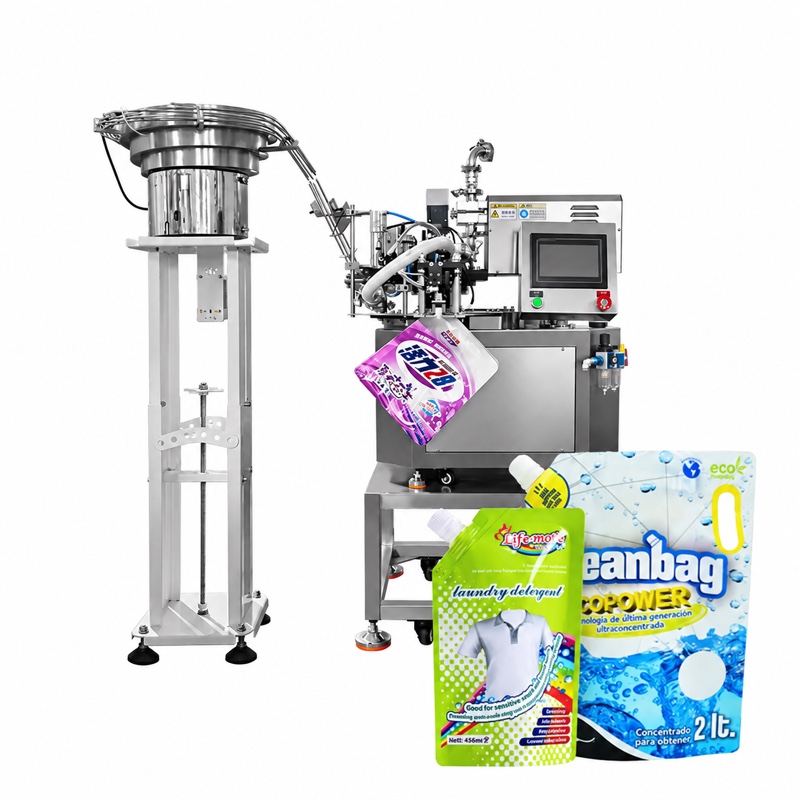
- Compact production rooms needing an all-in-one automatic bag-loading, lid-feeding, and lid-screwing footprint (1400 × 900 × 1050 mm, 100 kg).
- Choke-safe tamper-evident screw caps sorted automatically via vibratory feeder bowl.
Better-Matched Sibling Configurations
Higher-speed 20–70 bags/min top-filled premade stand-up pouches without screw spouts
LV-210 Premade Stand-Up & Zipper Pouch Machine →High-output tear-top gel sticks or 4-side sachets (80–640 packs/min across 2–16 lanes)
LV-500SY / 700SY / 980SY Multi-Lane 4-Side Sachet Machine →Wide-mouth single-serve jelly cups sealed with roll-film easy-peel lids
Automatic CIP Jelly Cup Fill-Seal Machine →
Specification Table (Metric & Imperial)
| Parameter | Metric Specification | Imperial Equivalent | Operating Condition & Verification Note |
|---|---|---|---|
| Model | LV-160 | — | LINEVO T04 automatic spout-pouch filling and capping machine. |
| Packing Speed | 10–15 bags/min | — | Depends on product viscosity, fill volume (e.g., 100 ml jelly vs. up to 2 kg/5 L liquids), and pack size. |
| Power & Voltage | 3 kW · 220V/380V 50Hz | — | Give voltage, phase, and frequency at your site; quotation states electrical configuration. |
| Machine Weight | 100 kg | 220 lb | Net machine weight; shipping weight and crate size stated with order. |
| Machine Size | 1400 × 900 × 1050 mm | 55.1 × 35.4 × 41.3 in | Length × width × height; layout drawing in quotation shows floor space with cap feeder stand. |
Shift Production Reality Note: Listed cycle speeds depend on container or bag volume, target fill weight, and material flow characteristics. For multi-shift plant planning, multiply nominal run rate by a 0.70–0.85 shift OEE factor (accounting for film/label splices, hopper refills, and routine cleaning) and confirm exact speed with your samples during Foshan FAT.
What Is Included vs. What We Review With You
Core Station Scope
- Automatic spout-rail bag loading, through-spout liquid/gel filling nozzle, vibratory cap feeder bowl, automatic lid placement, and automatic lid screwing
- Finished spout-pouch discharge chute in compact 1400 × 900 × 1050 mm frame
Reviewed Against Your Samples & Plant
- Application contact materials (food/sanitary SUS304/316L seals and heated hopper if hot-filling drinking jelly vs. ambient liquids)
- Spout neck rail track width (e.g., 8.6 mm, 10 mm, or 16 mm spout fitment) and cap chuck profile matched to your cap samples
- Fill cylinder volume range and plant electrical supply (220V/380V, 50/60 Hz)
Verified Electrical, Sensing & Pneumatic BOM
PLC Motion & Sequence Controller
Main programmable logic controller coordinating multi-lane rotary piston dosing, film/cup indexing, jacket heating, and sealing interlocks.
Rotary Encoder, Control Relays & 24V Switching Power Supply
Phase-angle timing feedback, cabinet switching relays, and regulated 24V DC power supply across multi-lane stick, sachet, and cup stations.
HMI Color Touchscreen & Variable Frequency Drive (VFD)
Multi-recipe touchscreen terminal storing lane dose/temperature profiles and inverter motor speed control for main drives and conveyors.
Pneumatic Cylinders, Solenoid Valves, Vacuum Gauge & FRL Unit
Suck-back anti-drip nozzle actuators, cross-sealing cylinders, manifold valves, pouch-opening vacuum gauge, and air preparation unit.
Representative electrical, sensing, and pneumatic hardware fitted on LINEVO packaging configurations; exact part series or project-specified alternatives are itemized in your written quotation BOM.
How It Works & Mechanical Countermeasures to Common Line Failures
- 01Automatic Spout-Rail Bag Loading
Pre-spouted empty pouches slide by their plastic neck flanges into the indexing track.
- 02Through-Spout Volumetric Filling
The filling nozzle seals onto the spout mouth to inject drinking jelly or liquid without air pockets or exterior drips.
- 03Automatic Vibratory Lid Feeding
The overhead bowl orients tamper-evident screw caps and feeds one cap onto each filled spout.
- 04Torque-Controlled Lid Screwing & Output
The rotary chuck screws the cap down to consistent tamper-band engagement before ejecting the finished pouch.
Production Floor Failure Modes & LINEVO Countermeasures
Cross-Threaded Choke-Safe Caps Leaking Inside Pasteurization Baths
Floor Risk: Hand-capping or unaligned chucks cock tall baby/jelly safety caps sideways, failing squeeze tests.
Mechanical Countermeasure: Rigid spout-neck rail clamping holds the plastic fitment vertical during automatic cap placement and rotary screwing.
Air Bubbles Foaming Inside Flexible Drinking-Jelly Pouches
Floor Risk: Splashing viscous konjac beverage through narrow 8.6 mm spouts traps headspace air that oxidizes fruit flavor.
Mechanical Countermeasure: Sealed through-spout nozzle dosing (plus optional pre-cap air evacuation reviewed per project) fills pouches smoothly.
Jelly Residue Drying Inside Spout Threads & Locking Caps
Floor Risk: Dripping nozzles leave sticky syrup on external neck threads.
Mechanical Countermeasure: Clean shut-off dosing through the spout bore keeps external threads dry before cap placement.
Scaling Beyond 15 Bags/Min When Retail Demand Doubles
Floor Risk: Single-nozzle LV-160 tops out at 10–15 bags/min.
Mechanical Countermeasure: Plants either bank two compact 100 kg LV-160 cells by flavor or step up to multi-nozzle rotary spout lines / LV-210 premade lines.
Comparing Quotations? Check These 5 Things
Multiply cycle rate (20–40 cuts/min) by lane count and a realistic 0.70–0.85 shift OEE factor accounting for hot-fill hopper replenishment, parent reel splices, and CIP sanitation.
Verify whether double-walled jacketed heating, mixing paddles, rotary-valve piston dosing, and pneumatic suck-back shut-off nozzles are sized for your gel viscosity and particulate size.
Confirm product-contact steel grade for acidic fruit gels, electrical heater load (kW, voltage/phase), and dry compressed air consumption (0.6–0.8 MPa) on the written scope sheet.
Check parent rollstock maximum width (420 / 500 / 700 / 980 mm), lane pitch, tear-notch punch geometry, and cup cavity rings against approved dieline drawings before plate engraving.
Require a filmed Foshan FAT running viscous gel or gummy samples at target fill temperature to verify zero seal-zone stringing, weight uniformity across lanes, and burst resistance.
From Sample Audit to Foshan FAT & Export Commissioning
- 01Sample Audit
Send physical containers, pouches, lids, film reels, or product specs to Foshan so engineers verify dimensions, flow behavior, and station geometry.
- 02Written Scope Freeze
Confirm exact model/lane count, included vs. project-reviewed modules, electrical/air utilities, and format parts in the technical quotation.
- 03Foshan Fabrication & Wiring
CNC machining, stainless frame assembly, PLC/HMI programming, and inline station synchronization inside LINEVO's 15,000+ m² Foshan plant.
- 04Foshan FAT Run Before Shipment
Full-speed trial on sample materials verifying registration, dosing/vacuum stability, seal integrity, and fault interlocks on video or in person.
- 05Export Crating & Commissioning
Fumigation-free export crating, English schematics, parameter backups, wear-part list, and remote video or scheduled on-site commissioning.
Frequently Asked Questions
Notice the catalog also lists up to 2 kg / 5 L liquid detergents—how is LV-160 configured for food drinking jelly?
LV-160 is LINEVO's modular spout-pouch chassis; for food drinking jelly and fruit purees (typically 80–250 ml), we fit sanitary food-grade stainless contact parts, smaller precision dosing cylinders, and chuck tooling matched to choke-safe beverage caps.
Can one LV-160 run different pouch body shapes?
Yes—because spouted pouches hang by their rigid plastic neck flange, pouches of different body volumes or die-cut shapes that share the exact same spout neck flange and cap run with minimal adjustment.
What samples are needed to build the vibratory cap bowl and rail?
Ship 100 empty spouted pouches and 200 matching screw caps so rail clearance, vibratory bowl tracks, and torque clutch settings are tested in Foshan.