What It Is Built For vs. When to Choose Another Configuration
Target Products & Production Duty
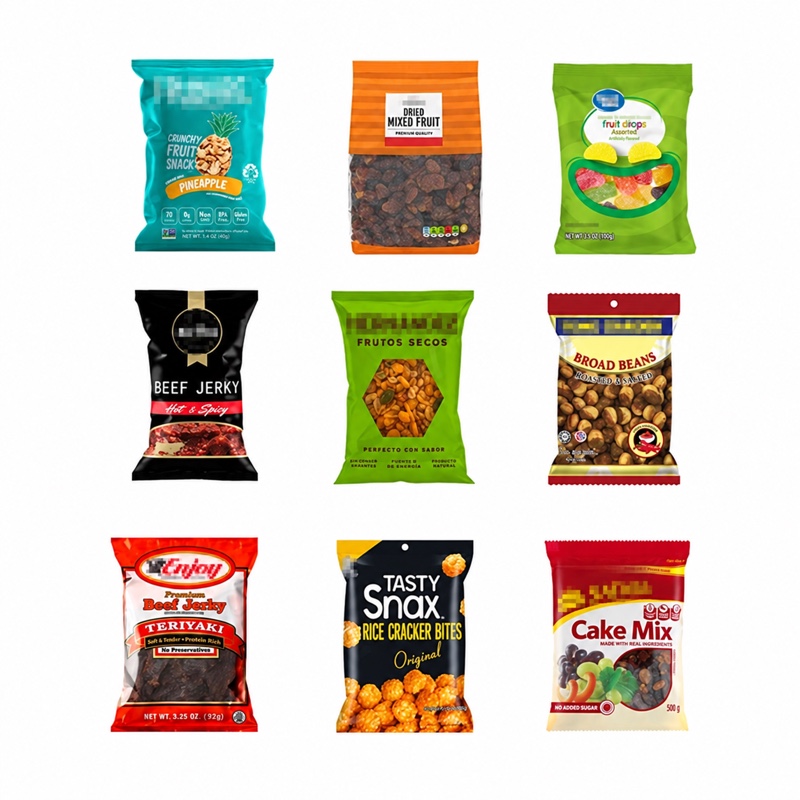
- Confectionery plants running high-volume pillow or side-gusset bags of gummy bears, fruit chews, jelly beans, and wrapped mini jellies from economical rollstock film.
- Hygroscopic pectin and gelatin formulations requiring hermetic multi-layer barrier film seals against moisture uptake, clumping, and melting.
- Bulk foodservice bags and high-speed retail packs where rollstock cost per bag beats premade pouches.
Better-Matched Sibling Configurations
Freestanding premade doypacks with resealable press-to-close zippers (90–210 mm wide)
LV-210 Premade Zipper Gummy & Multipack Machine →Direct liquid/hot-fill dosing of konjac jelly or sports gel into multi-lane stick packs
Multi-Lane Konjac & Energy Gel Stick Machine →Single-serve rigid PP/PET jelly and pudding cups with easy-peel lids
Automatic CIP Jelly Cup Fill-Seal Machine →
Specification Table (Metric & Imperial)
| Parameter | Metric Specification | Imperial Equivalent | Operating Condition & Verification Note |
|---|---|---|---|
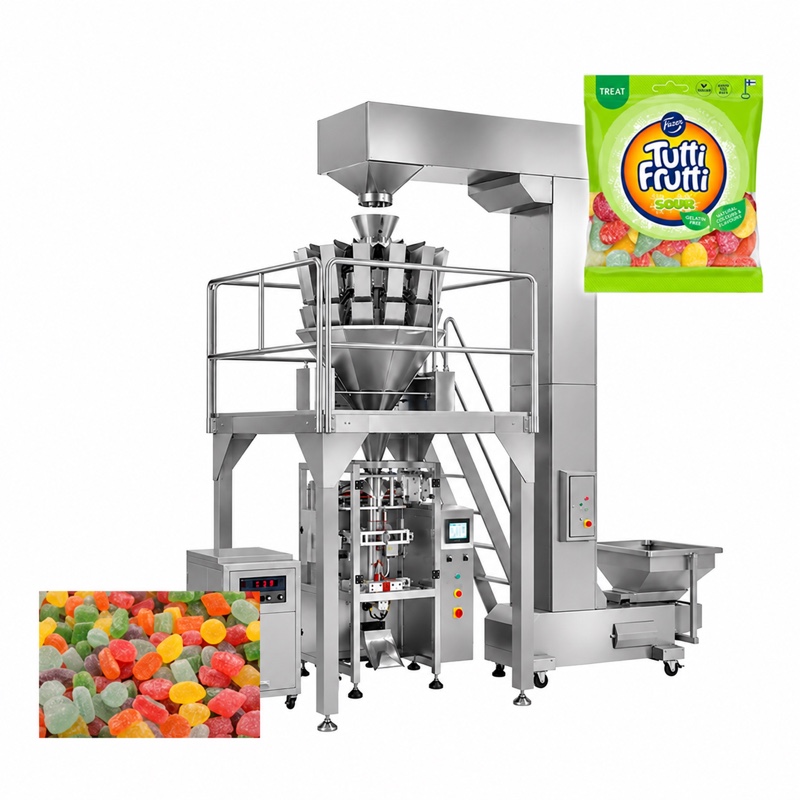
| Equipment Family | LINEVO T01 Heavy-Duty Confectionery VFFS Series | — | Complete Z-elevator + multihead weigher + vertical form-fill-seal tower. |
| Film Pull & Sealing Drive | Servo-driven film pulling + pneumatic cross-sealing mechanisms | — | Configured for multi-layer moisture-barrier confectionery films. |
| Target Products | Gummy candies, fruit chews, jelly beans, hard candies & jelly multipacks | — | Oiled vs. sanded sugar surface coating is tested on dimpled weigher pans in Foshan. |
| Bag Formats | Pillow bags & side-gusseted bulk/retail bags | — | Each bag width requires its dedicated stainless forming collar. |
| Speed, Bag Range & Utilities | Configured per target bag weight & ceiling clearance | — | Companion gummy VFFS setups run 30–70 bags/min depending on bag size; exact parameters stated in quotation. |
Shift Production Reality Note: Listed cycle speeds depend on container or bag volume, target fill weight, and material flow characteristics. For multi-shift plant planning, multiply nominal run rate by a 0.70–0.85 shift OEE factor (accounting for film/label splices, hopper refills, and routine cleaning) and confirm exact speed with your samples during Foshan FAT.
What Is Included vs. What We Review With You
Core Station Scope
- Stainless VFFS bagging unit with forming collar carriage, longitudinal sealer, and pneumatic cross-sealing jaws
- Servo-driven film pulling belt assembly
Reviewed Against Your Samples & Plant
- Servo-driven film pulling and pneumatic cross-sealing pressure tuned to your barrier laminate thickness
- Anti-sticking dimpled 10-head or 14-head multihead weigher, Z-bucket elevator, and stainless support platform
- Forming collars per bag width, inline TTO/ribbon date coder, and plant voltage/air supply
Verified Electrical, Sensing & Pneumatic BOM
PLC Motion & Sequence Controller
Main programmable logic controller coordinating multi-lane rotary piston dosing, film/cup indexing, jacket heating, and sealing interlocks.
Rotary Encoder, Control Relays & 24V Switching Power Supply
Phase-angle timing feedback, cabinet switching relays, and regulated 24V DC power supply across multi-lane stick, sachet, and cup stations.
HMI Color Touchscreen & Variable Frequency Drive (VFD)
Multi-recipe touchscreen terminal storing lane dose/temperature profiles and inverter motor speed control for main drives and conveyors.
Pneumatic Cylinders, Solenoid Valves, Vacuum Gauge & FRL Unit
Suck-back anti-drip nozzle actuators, cross-sealing cylinders, manifold valves, pouch-opening vacuum gauge, and air preparation unit.
Representative electrical, sensing, and pneumatic hardware fitted on LINEVO packaging configurations; exact part series or project-specified alternatives are itemized in your written quotation BOM.
How It Works & Mechanical Countermeasures to Common Line Failures
- 01Bucket Elevation & Anti-Stick Dispersion
Gummies or wrapped mini jellies ride the Z-bucket elevator to the top dispersion cone and dimpled radial feeders.
- 02High-Speed Combination Weighing
Multihead buckets calculate the closest gram combination instantaneously and drop cleanly down steep chutes.
- 03Servo Rollstock Tube Forming
Multi-layer moisture-barrier film pulls smoothly over the forming collar via servo belts and seals longitudinally.
- 04Pneumatic Hermetic Cross-Sealing
Pneumatic jaws clamp and fuse moisture-tight top/bottom seals before discharging finished bags.
Production Floor Failure Modes & LINEVO Countermeasures
Carnauba-Oiled or Humid Pectin Gummies Clinging Inside Weigher Buckets
Floor Risk: Sticky gummies hang up on flat metal hoppers, causing missed dumps and erratically underweight bags.
Mechanical Countermeasure: Pairing embossed anti-sticking dimpled radial pans, buckets, and steep chutes keeps tacky gummies moving cleanly.
Humidity Ingress Turning Bottled/Bagged Gummies Into One Fused Clump
Floor Risk: Weak fin or cross seams on thin OPP films let warehouse moisture sweat hygroscopic sugar/pectin gummies.
Mechanical Countermeasure: Servo film pulling handles thick metallized/high-barrier laminates while pneumatic cross jaws lock moisture-tight seams.
Bouncing Gummies Getting Crushed Inside Closing Cross-Seal Jaws
Floor Risk: Long vertical drop distances scatter stray pieces across the seal line on fast cycles.
Mechanical Countermeasure: Staggered weigher dump timing and product-settling dwell synchronize cleanly with jaw closure.
Bag Length Drift When Switching Printed Confectionery Rollstock
Floor Risk: Mechanical clutch pullers slip as roll diameter shrinks.
Mechanical Countermeasure: Servo-driven film pulling paired with photoelectric eye-mark tracking holds consistent cut registration.
Comparing Quotations? Check These 5 Things
Multiply cycle rate (20–40 cuts/min) by lane count and a realistic 0.70–0.85 shift OEE factor accounting for hot-fill hopper replenishment, parent reel splices, and CIP sanitation.
Verify whether double-walled jacketed heating, mixing paddles, rotary-valve piston dosing, and pneumatic suck-back shut-off nozzles are sized for your gel viscosity and particulate size.
Confirm product-contact steel grade for acidic fruit gels, electrical heater load (kW, voltage/phase), and dry compressed air consumption (0.6–0.8 MPa) on the written scope sheet.
Check parent rollstock maximum width (420 / 500 / 700 / 980 mm), lane pitch, tear-notch punch geometry, and cup cavity rings against approved dieline drawings before plate engraving.
Require a filmed Foshan FAT running viscous gel or gummy samples at target fill temperature to verify zero seal-zone stringing, weight uniformity across lanes, and burst resistance.
From Sample Audit to Foshan FAT & Export Commissioning
- 01Sample Audit
Send physical containers, pouches, lids, film reels, or product specs to Foshan so engineers verify dimensions, flow behavior, and station geometry.
- 02Written Scope Freeze
Confirm exact model/lane count, included vs. project-reviewed modules, electrical/air utilities, and format parts in the technical quotation.
- 03Foshan Fabrication & Wiring
CNC machining, stainless frame assembly, PLC/HMI programming, and inline station synchronization inside LINEVO's 15,000+ m² Foshan plant.
- 04Foshan FAT Run Before Shipment
Full-speed trial on sample materials verifying registration, dosing/vacuum stability, seal integrity, and fault interlocks on video or in person.
- 05Export Crating & Commissioning
Fumigation-free export crating, English schematics, parameter backups, wear-part list, and remote video or scheduled on-site commissioning.
Frequently Asked Questions
Should we pack gummies on this VFFS rollstock tower or the LV-210 premade zipper machine?
Choose VFFS when lowest film cost per bag and higher pillow-bag speed (up to 70 bpm on small packs) drive unit economics; choose LV-210 when marketing requires freestanding resealable press-to-close zipper doypacks.
What ceiling height is needed for the Z-elevator + multihead weigher + VFFS tower?
Complete tower height typically spans 3.4–4.2 meters depending on weigher size and VFFS frame; share your room clear height so LINEVO configures standard or low-profile inclined infeed layouts.
Can this VFFS pack individually sealed konjac sticks into 20-count outer bags?
Yes—counting/weighing sealed sticks or mini cups into pillow outer multipacks is a common secondary packaging configuration; send sample sticks for Foshan chute flow testing.